Safety equipment extraction lab compliance starts here. For how federal reclassification affects lab compliance requirements, see our Schedule III analysis. What does a cannabis extraction lab actually need? A compliant facility requires, at minimum: a classified electrical system (C1D1 or C1D2), continuous LEL gas detection with an alarm set at no greater than 25 percent of the Lower Explosive Limit, mechanical exhaust ventilation at a minimum of 1 CFM per square foot of floor area, method-appropriate personal protective equipment, a listed fire suppression system, and compliant flammable liquid storage. Skipping or cutting corners on any of these isn’t just a compliance failure. It is an explosion or asphyxiation waiting to happen. Across the cannabis and hemp industry, the same preventable failures appear again and again, and they always come back to operators who trusted vendor sales pages instead of compliance standards.
This guide covers every category of safety equipment required for a cannabis extraction lab, broken down by extraction method, with specific reference to NFPA 1, NFPA 70 (NEC), OSHA standards, and state-level fire code requirements. Use it as both an educational resource and a working pre-inspection checklist.
Understanding Hazardous Area Classification: C1D1 vs. C1D2
Before purchasing a single piece of equipment, you need to understand how your extraction room is classified under the National Electrical Code (NFPA 70, Article 500). This classification determines every piece of electrical hardware in the room, from light fixtures to outlets to motor starters.
Class 1, Division 1 (C1D1) applies to locations where flammable gases or vapors exist under normal operating conditions. If you are running a hydrocarbon extraction system with butane or propane, your extraction room is a C1D1 environment. Vapors are present every time the machine cycles. The solvent is inherently present in the space during normal operations.
Class 1, Division 2 (C1D2) applies to locations where flammable materials are handled in closed systems and vapors would only be present in abnormal circumstances, such as a container failure or accident. Closed-loop ethanol extraction in a well-ventilated room may qualify as C1D2 in some jurisdictions, but this determination must be made by a licensed engineer and confirmed with your Authority Having Jurisdiction (AHJ). Do not assume C1D2 is sufficient without that determination in writing.
The practical difference in required equipment is significant:
| Equipment Category | C1D1 Requirement | C1D2 Requirement |
|---|---|---|
| Electrical fixtures | Explosion-proof, listed for C1D1 | Explosion-proof or purged/pressurized |
| Motors and fans | Intrinsically safe or explosion-proof | Non-sparking or explosion-proof |
| Outlets and switches | All must be outside the classified area or explosion-proof listed | Explosion-proof or standard if outside classified boundary |
| HVAC controls | Intrinsically safe controls in classified zone | Standard controls acceptable outside boundary |
| Wiring method | Threaded rigid conduit or Type MI cable | Threaded rigid conduit, Type MI, or in some cases Type PLTC or ITC |
One of the most common and costly compliance failures is operators who build C1D2 rooms for butane extraction because it is cheaper. The AHJ will reject this. Butane vapor is heavier than air (vapor density approximately 2.0 relative to air), pools at floor level, and is present every time the extraction system vents or cycles. That is a C1D1 environment, period.
Related reading: How to Build an Extraction Lab: The Complete Step-by-Step Guide
Gas Detection and LEL Monitoring: The Most Critical Safety System in Your Lab
LEL stands for Lower Explosive Limit, the minimum concentration of a flammable vapor in air at which ignition can occur. For n-butane, the LEL is 1.8 percent by volume in air. For propane, it is 2.1 percent. For ethanol, it is 3.3 percent. These numbers are not theoretical. At these concentrations, a single spark, a light switch, or a static discharge can trigger an explosion.
Per NFPA 1 (Fire Code), Chapter 38 on cannabis extraction, your gas detection system must:
- Provide continuous monitoring of the extraction room atmosphere
- Trigger an audible and visual alarm when concentrations reach no greater than 25 percent of the LEL of the solvent in use
- Be connected to a non-interruptible power supply (the system cannot lose power during normal operations or a power disruption)
- Be listed and labeled for use in the classified environment
- Have sensors positioned at appropriate heights relative to the vapor density of the solvent
That 25 percent threshold is not a suggestion. It is the point at which your extraction system should trigger an automatic interlock to shut down the operation and your alarm must be sounding to evacuate personnel. At 50 percent LEL you are already in emergency territory with a rapidly closing window.
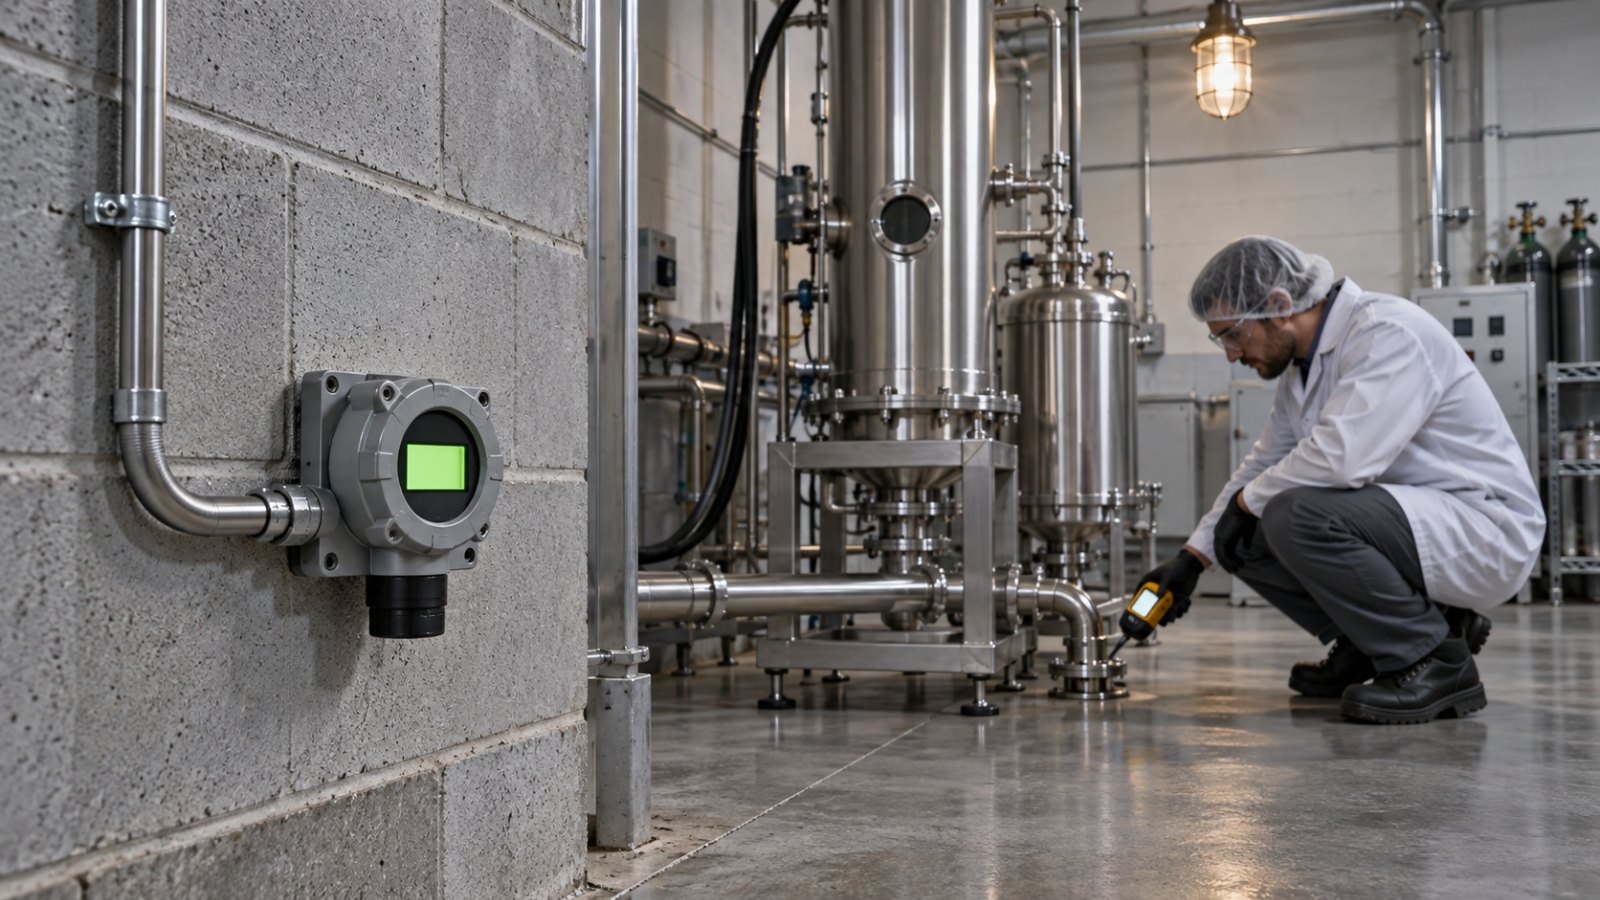
Sensor placement matters. Butane and propane are heavier than air. Sensors for hydrocarbon systems must be mounted low, typically 6 to 12 inches above the floor, where vapor will pool first. Ethanol vapor has a density close to air but still heavier at low temperatures; sensors should be mounted at or below mid-wall height. Mounting a butane sensor at head height is a common installation error that defeats the entire monitoring system.
Minimum sensor count for a standard extraction room:
- One fixed continuous monitor per classified room, mounted at correct height for solvent vapor density
- One additional fixed sensor for every 400 square feet of classified area in larger rooms
- At least one portable/personal monitor for each operator working in the space, for confined space entry and maintenance activities
Calibration requirements: Fixed LEL monitors must be bump-tested and calibrated per the manufacturer’s specification, typically every 6 months at minimum, and after any sensor replacement or known exposure event above alarm threshold. Document every calibration. Inspectors will ask for these records.
Do not use oxygen-depletion-based detectors as your primary gas detection for solvent-based extraction. Those are appropriate for CO2 extraction rooms where asphyxiation is the primary hazard, not for hydrocarbon or ethanol environments where the explosive hazard requires catalytic bead or photoionization detection technology.
What a High LEL Reading Actually Means: Reading Bands, Causes, and the Response at Each Level
The monitor on the wall reports percent of LEL, not percent of gas in the air, and the two get confused on every inspection walk-through. Butane’s LEL is 1.8 percent by volume, so 100 percent LEL is 1.8 percent butane, 10 percent LEL is 0.18 percent butane (1,800 ppm), and the 25 percent LEL alarm point is 0.45 percent butane (4,500 ppm). Propane’s 25 percent point is 5,250 ppm and ethanol’s is 8,250 ppm. One liter of liquid butane flashes to roughly 250 liters of vapor, and in a 1,000 cubic foot room that single liter is 0.9 percent by volume, half the LEL, before anyone has noticed the puddle. That is the scale the reading is warning you about.
| Reading (butane) | What it means | Likely cause | Required response |
|---|---|---|---|
| 0 to 5% LEL (0 to 900 ppm) | Baseline. A reading that sits at 2 to 4 percent and never returns to zero between runs is not baseline; it is a slow leak or a drifting sensor. | Normal fitting weep during a run; spent biomass off-gassing; zero drift. | Log the resting value each shift. Investigate any resting value above 2 percent with a portable at floor level. |
| 5 to 10% LEL (900 to 1,800 ppm) | Something is releasing solvent faster than the exhaust is removing it. | Open collection vessel, solvent transfer in progress, a purge vented into the room instead of the exhaust, a gasket starting to fail. | Boost exhaust to high speed. Stop introducing new solvent. Find the source with a portable before the number climbs. |
| 10% LEL (1,800 ppm) | The low alarm. OSHA 1910.146 defines a flammable atmosphere above 10 percent LEL as hazardous for entry, which is why 10 percent is the common pre-alarm setpoint. | Active leak at a pump seal, sight glass, or column clamp; a recovery pump discharging past a bad check valve. | Low alarm sounds, exhaust interlocks to maximum, solvent introduction stops. Operators locate the leak or leave. Nobody resets the panel to make the noise stop. |
| 25% LEL (4,500 ppm) | The high alarm NFPA 1 Chapter 38 and IFC Chapter 39 require. This is the trip point, not a warning. | Liquid solvent release, a failed hose, a relief valve lifting on an overfilled tank, an exhaust fan that quit during a run. | Interlock kills power to the extraction system, the solvent supply valve closes, everyone leaves. No switches, no phones, no re-entry until a portable reads below 10 percent and the source is known. |
| 50% LEL and above (9,000 ppm and up) | Emergency. The room can reach 100 percent LEL in minutes from a liquid leak. | Ruptured line, dropped cylinder, tank overfill with the relief venting inside. | Evacuate the building, call the fire department, isolate the solvent supply from outside the room if the shutoff is placed correctly. The reading has already told you the room is not survivable if it finds an ignition source. |
Notice what is missing from the response column: any step where an operator walks back in and clears the alarm. The interlock at 25 percent exists because the human reaction to an alarm is to go look, and looking means carrying a phone, a flashlight, and shoes with static charge into a room that is one spark from a deflagration. The reading tells you the concentration. The interlock takes the decision away from you.
Catalytic Bead, Infrared, or PID: What Your Sensor Can and Cannot See
The number on the panel is only as honest as the sensing element behind it, and the three technologies sold for extraction rooms fail in different directions.
| Sensor | How it reads | Butane / propane / ethanol response | How it fails | Right job |
|---|---|---|---|---|
| Catalytic bead (pellistor) | Burns the vapor on a heated catalyst bead and measures the temperature rise. | Reads all three, and every other combustible in the room, including hydrogen off a charging forklift battery. | Needs oxygen to burn; under-reads below about 10 percent O2. Silicone sprays, RTV sealant, sulfur compounds, and chlorinated solvents poison the bead, and a poisoned bead reads LOW. It looks healthy and misses the leak. | Fixed LEL monitoring when bump tests are actually done. Ban silicone aerosols from the room. |
| Infrared (NDIR) | Measures absorption of infrared light at the carbon-hydrogen bond wavelength near 3.4 microns. | Reads all three hydrocarbons, each with its own response factor; calibrate on the solvent in use or apply the manufacturer’s correction. Cannot see hydrogen. | Cannot be poisoned, works with no oxygen, and fails safe (a fouled optic reads as a fault, not as zero). Costs more per point. | Fixed monitoring in rooms where bump-test discipline is weak or solvent vapor is present most of the day. |
| Photoionization detector (PID, 10.6 eV lamp) | Ionizes vapor with UV light and counts the ions, in ppm. | Ethanol (ionization potential 10.47 eV) reads with a large correction factor; butane (10.53 eV) barely registers; propane (10.95 eV) does not respond to a 10.6 eV lamp at all. | A ppm instrument pointed at a percent problem. Zero response to propane means a propane room with a PID as its alarm has no alarm. | Hunting the leak after the fixed monitor says there is one. Never the primary LEL alarm. |
| Oxygen depletion | Electrochemical cell reads percent O2; alarms at 19.5 percent per OSHA. | Does not read combustibles at all. | Installed in a butane room as the “gas detector” because it was cheaper. It will read 20.9 percent while the room passes 25 percent LEL. | CO2 extraction rooms, where displacement is the hazard. |
False High or Real Leak: Diagnose Before You Reset
Most extraction rooms alarm weekly and the operators learn to reset the panel. That habit is how a real leak gets ignored on the one day it matters. Every alarm gets a cause written next to it, and the pattern of the reading tells you where to look.
| Reading pattern | Likely cause | Test | Fix |
|---|---|---|---|
| Climbs when the recovery pump starts, falls when it stops | Pump shaft seal or discharge fitting leaking under pressure | Soap solution on every fitting with the pump running; portable held at the seal | Replace the seal, re-torque fittings, check the pump oil for solvent dilution |
| Spikes the moment the material column is opened after a run | Residual solvent trapped in spent biomass | Watch the reading while the column sits under vacuum; if it settles, the biomass was the source | Vacuum-purge the column and let the reading settle before opening; move spent biomass to an exhausted bin or outside, never a lidded tote in the corner |
| Sits at 3 to 8 percent with no run in progress and never zeros | Slow leak at a sight glass gasket or valve packing, a spent-biomass bin off-gassing, or sensor zero drift | Portable sniff at floor level along every gasket and at the bin; if the portable reads zero everywhere, the fixed sensor has drifted | Replace the gasket or move the bin; re-zero and bump the fixed sensor if the portable found nothing |
| Rises during cleaning | Isopropanol or ethanol wipe-down vapor, a real combustible and not a fault | Stop wiping; the reading falls within minutes with the exhaust on | Clean with the exhaust on high, keep wipe solvent in a closed squeeze bottle, log the event so the record shows a cause |
| Alarms during a solvent tank fill or transfer | Hose or fitting leak, or a relief valve lifting on a tank filled past 80 percent | Stop the transfer; check the fill gauge; soap-test the transfer fittings | Fill by weight to 80 percent, replace the hose on a schedule, transfer only with exhaust on high |
| Fixed monitor never reaches alarm during a bump test | Poisoned or aged catalytic bead, the dangerous failure: it reads low, not high | Apply 50 percent LEL span gas; a healthy sensor alarms within the manufacturer’s response time | Replace the sensor, then find the silicone sealant, lubricant spray, or sulfur source that killed it |
| Jumps when the forklift or pallet-jack charger runs next door | Hydrogen from lead-acid charging drifting under the door; catalytic beads read it, infrared does not | Correlate the alarm log with the charger schedule | Move charging out of the adjacent space; a hydrogen leak is its own explosion hazard, so do not solve it by switching to a sensor that cannot see it |
| Drifts upward on hot, humid days and settles at night | Condensation on the sensing element or temperature drift outside the sensor’s rated range | Compare against a portable at the same spot; bump test | Re-zero, add the rain-and-splash guard the manufacturer sells, keep the sensor away from the exhaust-air discharge and any steam source |
Sensor Height by Solvent
A sensor reads the air it sits in, and every solvent in this business sinks. The mounting height that passes inspection is the one that matches the vapor density of what you actually run.
| Solvent or gas | Vapor density (air = 1) | Sensor | Mounting height |
|---|---|---|---|
| n-Butane | 2.0 | Catalytic bead or IR, %LEL | 6 to 12 inches above the floor, at the low point of the room |
| Propane | 1.5 | Catalytic bead or IR, %LEL | 6 to 12 inches above the floor |
| Ethanol | 1.6 | Catalytic bead or IR, %LEL | Low to mid-wall, never above the breathing zone; cold ethanol vapor is denser than the number suggests |
| Carbon dioxide | 1.5 | Oxygen depletion, %O2 | 12 to 18 inches above the floor; CO2 is not an LEL problem |
| Hydrogen (battery charging areas) | 0.07 | Catalytic bead, %LEL | At the ceiling, above the chargers; the one gas in the building that rises |
Bump Test vs Calibration: The Two-Minute Habit That Keeps the Alarm Honest
A bump test is a pass or fail: expose the sensor to span gas and confirm it alarms. A calibration adjusts the sensor so the number it reports matches the gas concentration applied. Portables get bumped before each day’s use, which is the ISEA position and the one inspectors quote. Fixed monitors get bumped monthly and calibrated every six months, or on the manufacturer’s interval if it is shorter, and after any exposure above the alarm point. Use a span gas at 50 percent LEL of the solvent you run, 0.9 percent butane or 1.1 percent propane, not the methane cylinder that came with the instrument, because a bead calibrated on methane and reading butane is reporting a number with a correction factor nobody wrote down. Record the date, the gas, the reading, and who did it. A calibration log with gaps in it reads to an inspector as a monitor that was not working during the gaps.
We run this exact drill in the extraction training course: trip the interlock on purpose with span gas and watch what the room does before the first real batch goes in. The walkthrough is at extractiontraining.com.
Ventilation: Calculating What Your Extraction Room Actually Needs
Ventilation serves two functions in an extraction lab: diluting solvent vapors below the explosive threshold and providing fresh air for worker health. Both requirements must be met simultaneously, and the more stringent requirement governs the design.
Most jurisdictions enforce a minimum mechanical exhaust rate of 1 CFM per square foot of floor area for solvent extraction rooms. This is a baseline from NFPA 1 and many state fire codes. Some AHJs require more depending on solvent volume and equipment configuration.
However, calculating ventilation by floor area alone is the wrong approach for a well-engineered lab. The correct method is a dilution ventilation calculation based on maximum solvent release rate:
- Determine the maximum amount of solvent that could be released in the worst credible scenario (typically a vent event or small leak from the largest vessel in the system)
- Calculate the vapor generation rate in CFM using the solvent’s vapor pressure at room temperature
- Apply the required safety factor (typically 10x to 100x the calculated dilution rate, depending on code and AHJ)
- The larger of this number or the 1 CFM per sq ft minimum governs your exhaust fan selection
Critical design requirements for extraction room ventilation:
- Exhaust must discharge to the exterior of the building, away from air intakes, property lines, and ignition sources
- Exhaust fans and motors must be rated for the classified environment (C1D1 or C1D2 as applicable)
- The system must be designed for continuous operation during extraction, not on-demand only
- Makeup air must be provided to prevent negative pressure issues. A room at extreme negative pressure will affect equipment performance and door sealing
- Exhaust ductwork must be constructed of non-reactive material and maintained free of obstructions
- A duct failure or fan failure must trigger a system alarm and extraction equipment interlock
For CO2 extraction rooms, the hazard profile shifts entirely to asphyxiation. CO2 is odorless and colorless. It displaces oxygen at high concentrations. Extraction rooms using supercritical CO2 systems require dedicated CO2 monitors calibrated to trigger alarms before oxygen levels drop below safe thresholds (OSHA minimum oxygen level: 19.5 percent by volume). CO2 is heavier than air and accumulates at floor level, which means low-mounted sensors and floor-level egress planning are critical.
Explosion-Proof Electrical Equipment Checklist
Every electrical component inside a C1D1 classified boundary must be specifically listed and labeled for that classification. “Explosion-proof rated” on a product spec sheet is not sufficient. The listing must specify the hazardous location class, division, and applicable gas group.
Butane and propane fall into Group D under NEC hazardous location classifications. Ethanol and acetone fall into Group D as well. CO2 extraction rooms are generally not classified as hazardous electrical environments absent co-located solvents.
Minimum C1D1 electrical equipment checklist for a hydrocarbon extraction room:
- All light fixtures: explosion-proof, listed for Class 1 Division 1, Group D
- All switches and controls: either located outside the classified boundary or explosion-proof listed for C1D1
- All outlet receptacles: explosion-proof or relocated entirely outside the classified zone (preferred)
- All motors: explosion-proof or intrinsically safe for C1D1, Group D
- All conduit: threaded rigid metal conduit with explosion-proof fittings at all boxes and terminations
- Emergency shutoff: panic-button style emergency stop for the extraction system, located outside the classified zone and accessible from the room egress path
- Control panels: located outside the classified zone whenever feasible, or built as purged/pressurized enclosures listed for C1D1
One of the most frequently cited compliance failures during state cannabis lab inspections is non-rated electrical equipment inside the classified zone. Common violations include standard LED shop lights installed by a general contractor who didn’t understand the classification, standard GFCI outlets installed for “convenience,” and non-rated extension cords run into the extraction room. Any of these can provide the ignition source for a catastrophic event.
Personal Protective Equipment by Extraction Method
PPE requirements are not one-size-fits-all. The correct PPE depends on the specific hazards present for each extraction method. Operators who wear the wrong PPE for their process are not protected; they have a false sense of security.
Hydrocarbon Extraction (Butane, Propane, Mixed Blends)
Primary hazards: flash fire, freeze burns from cryogenic liquid solvent, high-pressure vessel exposure.
- Flame-resistant (FR) clothing: Minimum NFPA 2112-compliant FR shirt and pants (or coverall) for all personnel in the extraction room during active operations. Standard cotton or polyester will ignite and melt onto skin in a flash fire event. FR cotton or Nomex are the baseline minimum.
- Chemical splash goggles: Not safety glasses. Goggles with a full seal against the face. Butane and propane exits the system as a rapidly expanding cryogenic gas that can freeze tissue on contact and cause permanent eye damage in under a second.
- Face shield: Over goggles when working on connections, fittings, or any component that could release solvent under pressure.
- Cryogenic gloves: For any direct handling of solvent supply cylinders or cryogenic-temperature connections. Standard chemical-resistant gloves do not protect against cryogenic burns.
- Chemical-resistant safety footwear: Closed-toe, chemical-resistant, static-dissipating or antistatic sole. No synthetic materials that can generate static discharge.
Ethanol Extraction
Primary hazards: chemical splash, inhalation of ethanol vapor, flash fire at high solvent volumes.
- FR clothing: Recommended for large-scale ethanol operations with significant open solvent exposure. Ethanol flash fires are less common than hydrocarbon events but possible at commercial scale.
- Chemical splash goggles: Required whenever handling bulk ethanol or working on transfer systems.
- Nitrile gloves (minimum): For routine operations. Thicker butyl rubber gloves for extended or high-concentration contact. Standard nitrile is not impervious to ethanol for prolonged exposure.
- Respiratory protection: If the room is not adequately ventilated, a half-face respirator with organic vapor cartridges is required for extended work. OSHA PEL for ethanol is 1,000 ppm; NIOSH IDLH is 3,300 ppm. Continuous ventilation should keep ambient levels well below PEL in a properly designed room.
CO2 Extraction (Supercritical and Subcritical)
Primary hazards: asphyxiation from CO2 release, high-pressure mechanical hazards, thermal burns from hot vessels.
- Personal CO2 monitor: Every operator in a CO2 extraction room should carry a personal CO2/O2 monitor. This is the single most important piece of PPE for CO2 operations. A CO2 release is silent and odorless; operators have no sensory warning before incapacitation.
- Standard safety glasses or goggles for mechanical operations.
- Insulated gloves for work on hot vessels or CO2 transfer at subcritical temperatures.
- No flash fire risk means FR clothing is not required, but standard lab coat or lab wear is recommended.
Solventless Extraction (Ice Water Hash, Rosin)
Primary hazards: thermal burns from rosin presses, musculoskeletal from physical process work, wet/slippery surfaces from ice water operations.
- Insulated gloves: For rosin press operations. Plates operate at 160 to 220 degrees Fahrenheit.
- Non-slip footwear: Ice water hash work involves wet floors. Slip hazards are the leading injury mechanism in solventless rooms.
- No vapor inhalation hazard; standard ventilation for temperature and humidity control is sufficient.
Fire Suppression Systems
Standard wet sprinkler systems are not appropriate as the sole fire suppression method in solvent-based extraction rooms. Water can spread burning liquid solvents and cause additional hazards. Your safety equipment extraction lab fire suppression strategy must match the hazard:
- FM-200 (HFC-227ea) clean agent suppression: The most common system used in hydrocarbon and ethanol extraction rooms. Suppresses fire without damaging equipment, does not create conductive liquid, and is safe for occupants at design concentrations. Requires a fire-rated enclosure with proper door sealing to hold suppression agent.
- CO2 total flooding: Effective but requires immediate evacuation before discharge; not recommended where personnel may be present during a fire event.
- Portable fire extinguishers: Class B:C dry chemical or CO2 extinguishers must be positioned at every egress from the extraction room. Minimum one extinguisher with a minimum 10-pound agent capacity. ABC dry chemical extinguishers are NOT preferred in equipment-intensive labs because the residue damages precision equipment.
- State-specific requirements: Many state cannabis fire codes require AHJ review and approval of the suppression system design before installation. Coordinate with your fire marshal early.
Flammable Liquid Storage Compliance
How and where you store your hydrocarbon or ethanol solvent supply is governed by NFPA 30 solvent storage rules (Flammable and Combustible Liquids Code) and your local fire code. Common violations and correct practice:
- Flammable liquid storage cabinets: All quantities of flammable liquids not in immediate use must be stored in listed flammable storage cabinets (FM or UL listed). These cabinets limit the quantity that can be stored outside a dedicated storage room and provide a minimum 10-minute fire resistance for the contents.
- Maximum quantities by occupancy: NFPA 1 and IBC (International Building Code) establish maximum allowable quantities (MAQs) of flammable liquids per control area. Exceeding these quantities without a High-Hazard Occupancy designation and the associated building construction requirements is a code violation. Work with your fire protection engineer to determine your MAQ.
- Hydrocarbon gas cylinders: Butane and propane cylinders in use must be secured upright, away from heat sources, and in the minimum quantity required for operations. Excess cylinders must be stored in a compliant outdoor cage or separated storage area.
- No storage near exits or means of egress: Flammable liquid containers may not obstruct or be positioned within 10 feet of exit doors or corridors in most codes.
- Bonding and grounding: All metal containers and transfer equipment must be bonded and grounded during liquid transfers to prevent static ignition.
Emergency Equipment and Spill Response
Every extraction lab, regardless of method, must have the following emergency equipment accessible and maintained:
- Emergency eyewash station: ANSI Z358.1 compliant, within 10 seconds of travel from any area where chemical splash can occur. Must deliver tepid water at a minimum of 0.4 GPM for 15 continuous minutes. Plumbed stations are preferred; portable units must be inspected and refilled weekly.
- Emergency shower: Required if full-body chemical contact is possible. For most extraction operations, an eyewash station at minimum and a shower for bulk solvent handling operations.
- Spill containment: Secondary containment for all flammable liquid storage and transfer areas. The containment must be capable of holding 110 percent of the volume of the largest single container, or 10 percent of the total stored volume, whichever is greater.
- Spill kit: Non-sparking sorbent materials appropriate for the solvents in use. Standard clay-based absorbents are acceptable for ethanol. Non-sparking plastic or stainless steel scoops only. No steel brushes or tools that can generate sparks in a solvent spill response.
- Evacuation plan and signage: Posted exit routes, assembly point, and emergency contact information. OSHA 29 CFR 1910.38 requires a written emergency action plan for all facilities with more than 10 employees; smaller operations should maintain one regardless.
Safety Equipment Extraction Lab Compliance Checklist: Pre-Inspection Summary
Before your first state inspection or a scheduled compliance audit, walk through this checklist:
Electrical and Classification
- Room classification determination documented and stamped by licensed engineer
- All electrical equipment inside classified zone listed for correct class, division, and gas group
- All conduit seals filled and in place
- No unapproved modifications to electrical system since last inspection
Gas Detection
- Fixed LEL monitors installed at correct height for solvent vapor density
- Alarm threshold set at 25 percent LEL or less
- Calibration records current and on file
- Interlocks verified functional (alarm triggers extraction system shutdown)
- Backup power confirmed
Ventilation
- Exhaust rate meets 1 CFM per sq ft minimum
- Exhaust discharges to exterior, away from intakes and ignition sources
- Fan failure alarm functional
- Makeup air supply balanced
PPE
- FR garments available in correct sizes for all extraction personnel
- Chemical splash goggles at every workstation
- Appropriate gloves stocked and accessible
- Personal gas monitors charged and calibrated (CO2 rooms or confined space entry)
Fire Suppression and Emergency Equipment
- Fire suppression system inspected within last 12 months (service tag on panel)
- Portable fire extinguishers at every egress, inspected monthly and serviced annually
- Eyewash station within 10-second travel of hazard area, tested weekly
- Spill kit stocked and accessible
- Emergency action plan posted
Storage and Chemical Management
- All flammable liquids in listed storage cabinets or compliant storage room
- Quantities below MAQ for occupancy classification
- Bonding and grounding cables present on all transfer points
- SDS sheets accessible for all chemicals on-site
Common Safety Equipment Extraction Lab Mistakes and How to Fix Them
Mistake: Relying solely on vendor-provided compliance claims. Equipment vendors sell booths labeled “C1D1 compliant,” but compliance of the room depends on the entire installation, not just the booth itself. The electrical wiring, lights, and HVAC serving that booth must also be correctly classified. Fix: Get a hazardous location review from a licensed electrical engineer before finalizing your installation.
Mistake: Treating LEL monitors as set-and-forget equipment. Sensors degrade. Catalytic bead sensors lose sensitivity over time, especially when exposed to silicone vapors or high solvent concentrations. A monitor that reads zero may be reading zero because its sensor is dead. Fix: Bump test monthly, calibrate every 6 months, and replace sensors on the manufacturer’s recommended schedule.
Mistake: Under-sizing ventilation to save HVAC costs. Extraction rooms that run warm and accumulate vapor smells between batches are not adequately ventilated, regardless of what the CFM rating on the fan says. Fix: Commission the ventilation system with a smoke test or flow measurement to verify actual room air changes per hour and exhaust capture efficiency.
Mistake: Using standard nitrile gloves as the sole hand protection for hydrocarbon operations. Nitrile provides no meaningful protection against cryogenic liquid butane contact. Fix: Keep cryogenic gloves at every connection point where liquid solvent could discharge.
Mistake: Storing excess solvent cylinders inside the extraction room. More cylinders in the room means more fuel in a fire scenario. Fix: Store only the minimum cylinders required for current operations inside. Keep the balance in a compliant exterior storage cage.
Related Reading from WKU Consulting
- How to Build an Extraction Lab: The Complete Step-by-Step Guide
- Cannabis Winterization: The Complete Dewaxing Guide
- Wiped Film Distillation: Cannabis Oil Purification Guide
- Cannabis Devolatilization: Vacuum Oven Purging and Terpene Preservation
- Cannabis Remediation Decision Matrix: When to Save vs. Scrap Failed Batches
When a lab should upgrade safety equipment immediately
- Repeated nuisance alarms with no root-cause closure
- Operators bypassing interlocks to keep production moving
- Solvent odors showing up outside intended process areas
- No recent detector calibration records
- Unclear relief-device sizing or discharge routing
- Flammable liquid storage expanding beyond the original room design
- New equipment added without a fresh hazard review
- Shift leads giving different answers about shutdown procedure
Those are not minor operational quirks. They are warning lights that the process has drifted away from controlled design.
Before you buy anything, answer these design questions
- What solvent inventory is actually in the room during normal production? Safety equipment sizing should follow real inventory, not the number on an old startup slide.
- Where can vapor or gas accumulate first? Detector height and exhaust placement depend on this answer.
- Which tasks create the highest upset risk? Solvent transfer, gasket changes, warm equipment opening, and cleaning often deserve more attention than steady-state extraction.
- What happens if utility power drops mid-run? Shutdown logic should already account for that event.
Those questions keep a lab from buying generic hardware that looks sophisticated but does not actually match the process.
How to audit whether your lab’s safety equipment is actually adequate
- Map the solvent path. Where is solvent stored, transferred, processed, recovered, sampled, cleaned, and discarded?
- Map the pressure path. Which vessels, lines, valves, and fittings can see pressure, and what protects each segment?
- Identify ignition sources. Electrical, static, hot surfaces, friction, heaters, and non-obvious maintenance tools all count.
- Check detection placement. Are sensors located where the gas will actually accumulate or travel first?
- Check shutdown logic. What exactly happens when alarms trip or an operator hits E-stop?
- Check emergency access. Can an exposed worker reach eyewash, shower, exit, or alarm without crossing the hazard?
- Review maintenance records. If a safety layer is not inspected or calibrated, assume it is weaker than you think.
If you cannot answer those questions clearly, the gap is not just documentation. It is process understanding.
Speccing the safety envelope is where an extraction lab consultant earns the fee, and where an equipment list alone leaves gaps.
If you are speccing safety systems for a real build and not just making a list, this is where the expensive mistakes live: a misclassified space, a ventilation design that fails inspection, a six-figure redesign after the AHJ walks through. Designing extraction facilities so that does not happen is what WKU does. If you want that on your project before the concrete is poured, here is how to work with us.
Frequently Asked Questions
Does every cannabis extraction lab need a C1D1 room?
Not every method requires C1D1. Hydrocarbon extraction (butane, propane) requires C1D1 because flammable vapors are present under normal operating conditions. Supercritical CO2 extraction does not create a classified flammable atmosphere. Ethanol extraction may qualify as C1D2 or unclassified depending on the system design and solvent quantities; this determination must be made by a licensed engineer and confirmed with your AHJ. Never assume your classification without a formal review.
At what LEL percentage should an extraction lab alarm trigger?
Per NFPA 1, the alarm must trigger at no greater than 25 percent of the LEL. For butane (LEL 1.8% by volume), the alarm must sound before concentrations reach 0.45 percent by volume in air. At 25 percent LEL you still have a four-fold safety margin before the atmosphere becomes ignitable, but that margin closes rapidly in a confined space with an active leak.
What is the minimum ventilation rate for a cannabis extraction room?
Most codes require a minimum of 1 CFM per square foot of floor area for closed-loop solvent extraction rooms. This is a minimum, not an engineering target. A properly designed extraction room should be ventilated based on the actual vapor generation rate of the equipment inside it, which often exceeds the 1 CFM per sq ft minimum for larger systems.
Can I use CO2 fire extinguishers in a hydrocarbon extraction room?
CO2 extinguishers are effective for Class B fires (flammable liquids) and do not leave residue that damages equipment. They are an acceptable choice for extraction rooms. However, discharging a CO2 extinguisher in a confined space also creates an asphyxiation hazard for personnel. Ensure any operator trained to use a CO2 extinguisher understands this risk and is not trapped in an enclosed space during discharge.
What PPE is required for hydrocarbon extraction operators?
At minimum: flame-resistant (FR) clothing (NFPA 2112 compliant), chemical splash goggles, face shield for work on fittings or connections, cryogenic gloves for direct solvent cylinder handling, and antistatic chemical-resistant footwear. Standard cotton work wear is not acceptable. Polyester and synthetic materials are actively hazardous in a flash fire scenario because they melt onto skin.
Do I need a fire suppression system in my extraction room?
Yes. Most state cannabis codes and local fire codes require a listed suppression system in rooms where Class I flammable liquids are processed above certain quantities. The type of system required depends on your jurisdiction and occupancy classification. Clean agent systems (FM-200) are the standard choice for equipment-intensive extraction rooms because they suppress fire without water damage. Confirm requirements with your AHJ before construction.
How often do LEL monitors need to be calibrated?
Fixed LEL monitors should be bump tested monthly at minimum and fully calibrated every 6 months, or more frequently if the manufacturer specifies. Portable personal monitors should be bump tested before every shift. Calibration records must be maintained on-site; inspectors routinely request them during compliance audits.
Which agency does the auditing, and what the application and facility standards are in each of 41 states, is compiled in our cannabis extraction license requirements by state guide.
What happens if my extraction lab fails a safety inspection?
Depending on the violation severity, the AHJ or state cannabis regulatory body can issue a Notice of Violation with a cure deadline, issue a stop-work or cease-operations order for high-hazard violations, or in egregious cases, initiate license revocation proceedings. Immediate life-safety violations (missing or non-functional LEL monitoring, classified electrical violations, blocked egress) typically trigger immediate stop-operations orders. Correct paperwork violations (missing calibration records, expired extinguisher tags) are typically correctable with a short cure period.
What does 10 percent LEL mean in an extraction room?
Ten percent of the lower explosive limit, not 10 percent gas. For butane (LEL 1.8 percent by volume) that is 0.18 percent butane in air, or 1,800 ppm. OSHA 1910.146 treats a flammable atmosphere above 10 percent LEL as hazardous for entry, which is why most panels use it as the low alarm: exhaust goes to high, solvent introduction stops, and someone locates the source with a portable. The 25 percent LEL high alarm (0.45 percent butane, 4,500 ppm) is the point where the interlock shuts the system down and the room is evacuated.
Why does my LEL monitor alarm when I open the material column?
Spent biomass holds residual solvent after the recovery cycle, and opening the column releases it into the room at floor level where the sensor sits. Pull the column down under vacuum and watch the fixed reading settle before you crack the clamp; if the reading climbs while the column is still sealed, the leak is a gasket, not the biomass. Spent material goes to an exhausted bin or outside, never a lidded tote in the corner of the classified room.
Can a gas detector read high without a leak?
Yes. Isopropanol or ethanol wipe-downs, aerosol lubricants, hydrogen drifting in from a lead-acid battery charger, and condensation or temperature drift on a catalytic bead all raise the reading without a solvent leak. The bump test settles it: a sensor that alarms cleanly on 50 percent LEL span gas is reporting the room honestly. The failure to fear is the opposite one, a bead poisoned by silicone sealant that reads low and looks fine right up until it misses a real release.
One System, Proven Before the First Batch
The safety equipment in your extraction lab is not a compliance checkbox. It is the difference between a profitable operation and a catastrophic event that ends careers, destroys businesses, and injures people. The vendor pages that dominate search results for this topic will tell you their booth or their monitor is all you need. It is not. A compliant, safe extraction lab is a system: classified electrical infrastructure, calibrated gas detection, engineered ventilation, appropriate PPE, functioning suppression, and compliant storage all working together.
Get the system right from the start. Fix it before an inspector finds it. And when in doubt, call a licensed fire protection engineer and a hazardous location electrical engineer before you commit to a design.
For more on building and operating a compliant cannabis extraction lab, subscribe to the WKU Consulting YouTube channel and join our professional community on Discord.
Stay connected:
Newsletter: Subscribe to WKU Consulting Updates
Discord: Join the WKU Professional Community
Safety hardware only makes sense when it is matched to the actual extractor design. If you need the process-side breakdown of how hydrocarbon solvent moves, recovers, and creates pressure risk, read Closed-Loop Extraction Systems for Cannabis: How They Work, What Matters, and What Fails.
Safety gear only works inside a facility that was designed around the real solvent hazard, operator movement, ventilation burden, and emergency response path. For the full facility-side picture, read this cannabis extraction lab design guide before finalizing your room layout or equipment placement.
